Key takeaways
- An induction furnace melts metal with a magnetic field rather than a flame: a converter feeds a water-cooled coil, the coil's alternating field induces currents in the charge, and the metal heats and melts from the inside.
- The system has two parts. The IGBT converter is the brain: it converts the alternating current to the frequency and power the coil needs, and in doing so ensures optimal furnace performance. The melting unit is the muscle: it converts electrical energy into a magnetic field that heats and melts the metal through the principle of electromagnetic induction.
- Because the heat is made inside the metal with no combustion, induction melting is clean, recovers the full charge including scrap, runs at high energy efficiency and holds temperature under precise digital control.
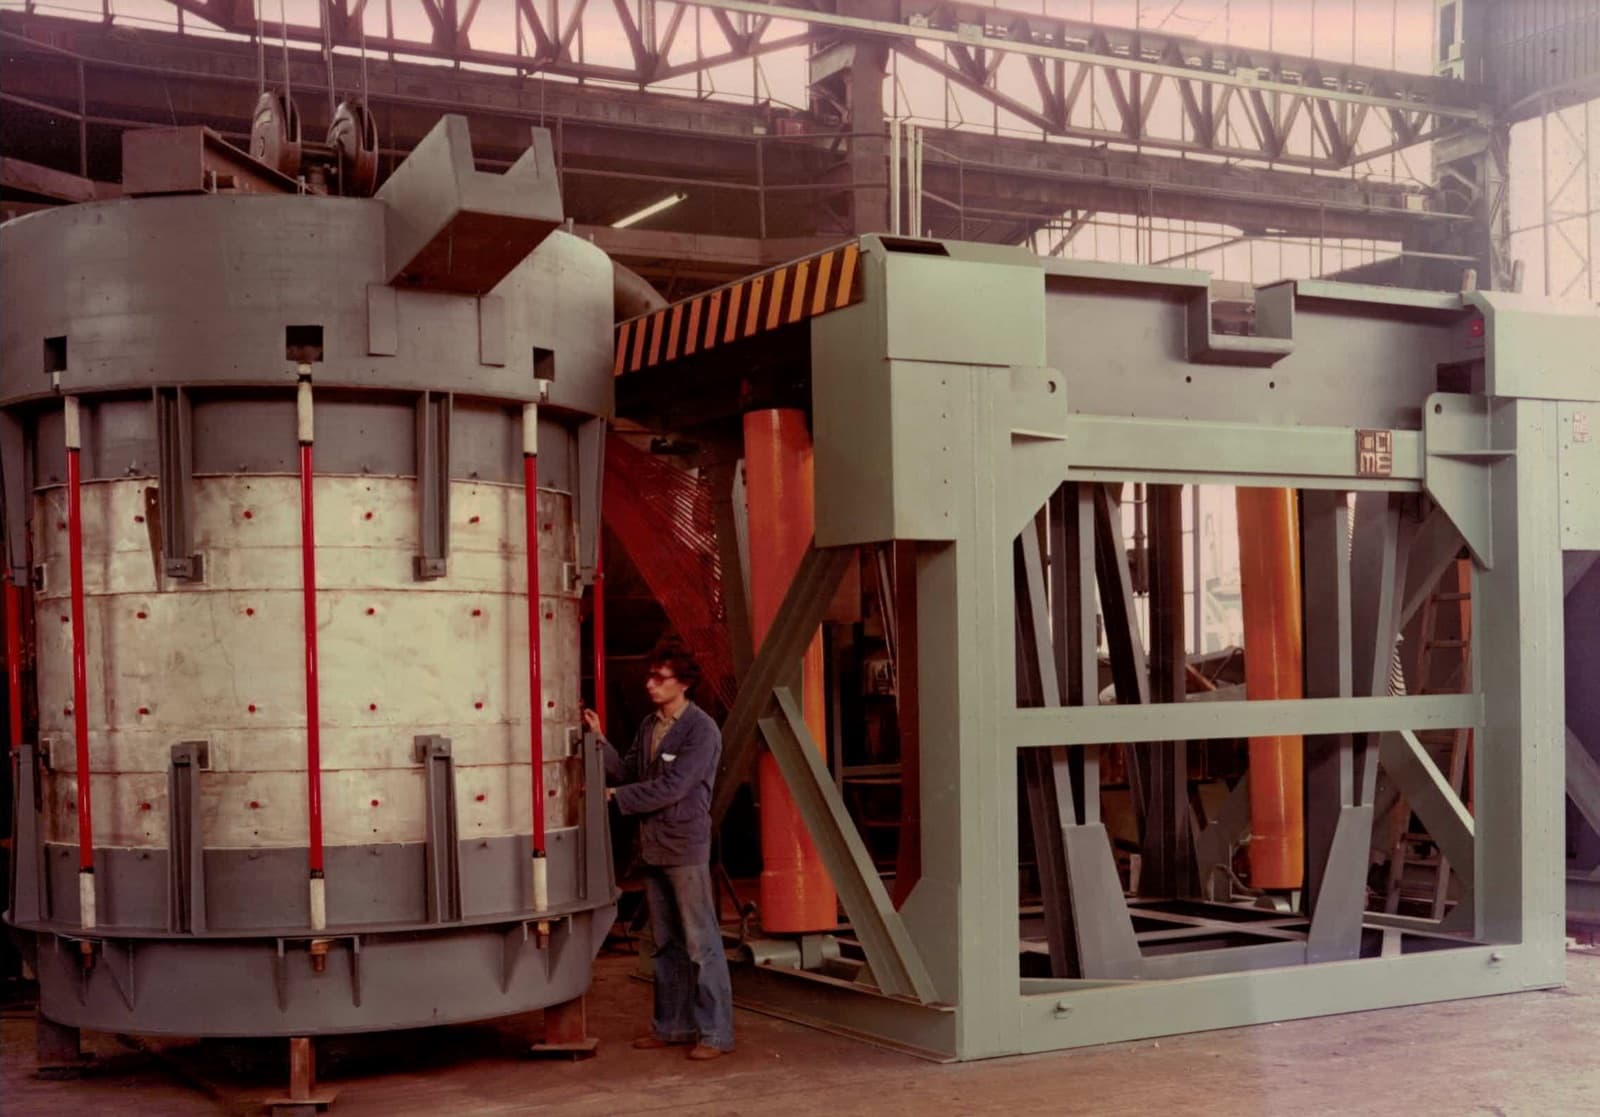
- Most foundry melting is done in coreless induction furnaces, which heat and, where required, stir the whole bath and empty completely for easy alloy changes. CIME has engineered coreless induction furnaces in Turin since 1952.
What an induction furnace does
An induction furnace melts metal with electricity, not with a flame. Where a cupola or a fuel-fired furnace burns fuel and transfers the heat to the metal from outside, an induction furnace uses a magnetic field to generate the heat inside the metal itself. There is no burner, no combustion and no flame touching the charge. That single difference is the reason many foundries melt iron, steel, copper and aluminium this way.
The way it works is simple. A charge of cold metal, scrap, foundry returns and fresh alloy, is loaded into a crucible wrapped in a copper coil. Power is switched on, the coil sets up an alternating magnetic field, and within minutes the metal begins to heat up, soften and melt into a bright liquid bath. The furnace holds that bath at a controlled temperature until it is ready to pour. In this article we go through all the steps that explain how an electric induction furnace works.
Note
An induction furnace does not heat the metal and then wait. It generates the heat and ensures uniform heating throughout the batch of metal, which can be held, stirred (if required) and corrected while it is liquid. That is what makes it both fast and controllable.
The principle: heat from a magnetic field
The physics behind it is the principle of electromagnetic induction, the effect Michael Faraday described in 1831: a changing magnetic field induces an electric current in any conductor nearby. An induction furnace puts that law to work. Alternating current in the coil creates an alternating magnetic field and, in doing so, heats and melts the metal directly inside the crucible. The metal charge inside the coil is a conductor, so the changing field induces circulating currents in it, called eddy currents.
Those eddy currents are where the heat comes from. The metal resists them, and that resistance turns the electrical energy straight into heat. Unlike a flame, which transfers heat from outside, induction generates the heat directly inside the metal: heating is therefore fast, uniform and free of losses.
The converter's frequency also affects the depth of heating (the higher it is, the thinner the layer involved), so it has to be matched to the size of the furnace and the type of metal. The same field does a second useful job. As it heats the bath, it also sets the molten metal inside in motion. This electromagnetic stirring mixes alloy additions evenly and levels out the temperature across the bath, so a sample taken from the top is the same as one from the bottom. A fuel-fired furnace has to rely on the metal's own slow convection to do the same thing. For how the coil and the coreless structure are built, see the core technology.
Two parts: the brain and the muscle
An induction furnace is really two machines working together.
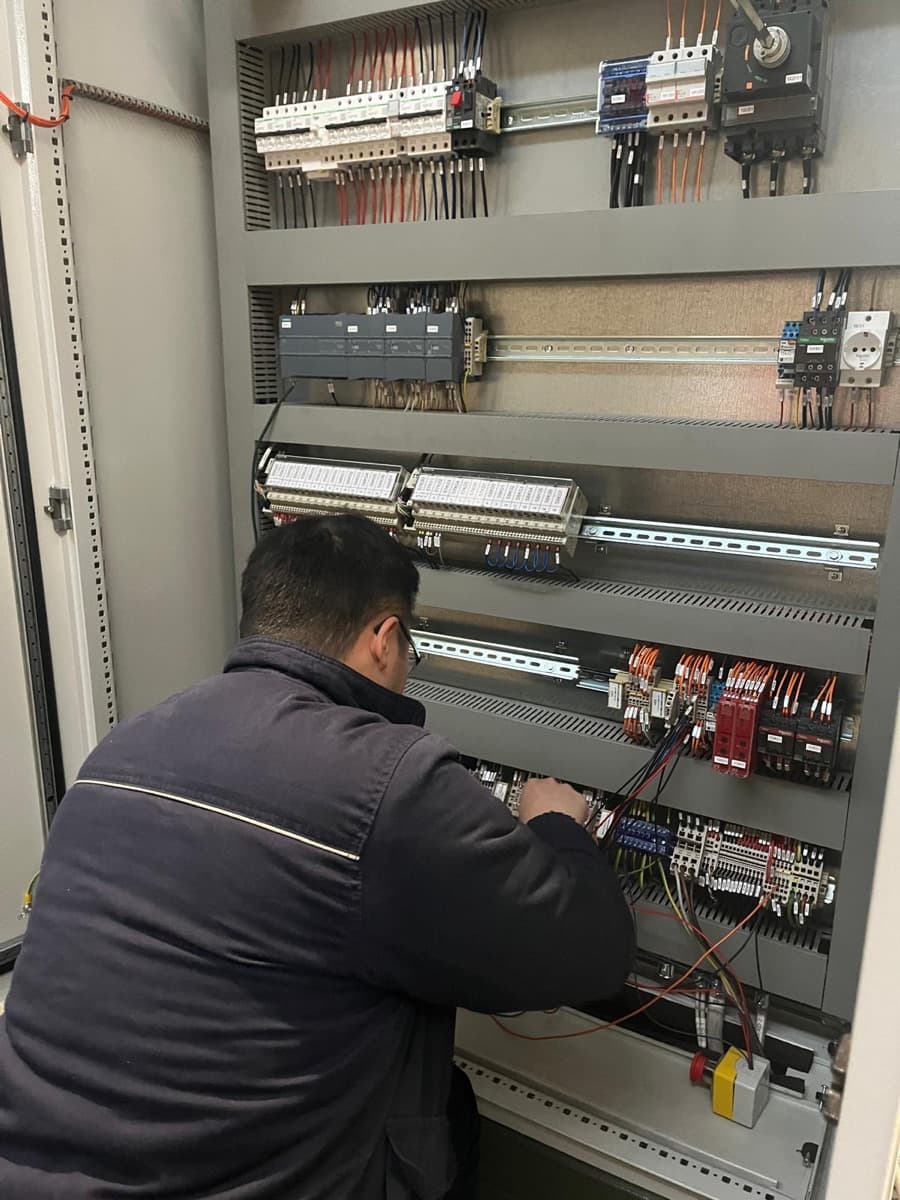
The power converter is the brain. It converts the alternating electrical current into direct current and reshapes it into alternating current at the frequency (medium frequency) the coil needs and at the power level the metal to be melted calls for. A modern converter uses IGBT switches, fast semiconductor devices that turn the current on and off thousands of times a second to set frequency and power precisely. This is how the metal is managed: the converter holds the power steady as the charge changes state. To learn more, see the IGBT power electronics page, and to understand the differences between a modern IGBT converter and an earlier-generation SCR one, see the article IGBT vs SCR converters.
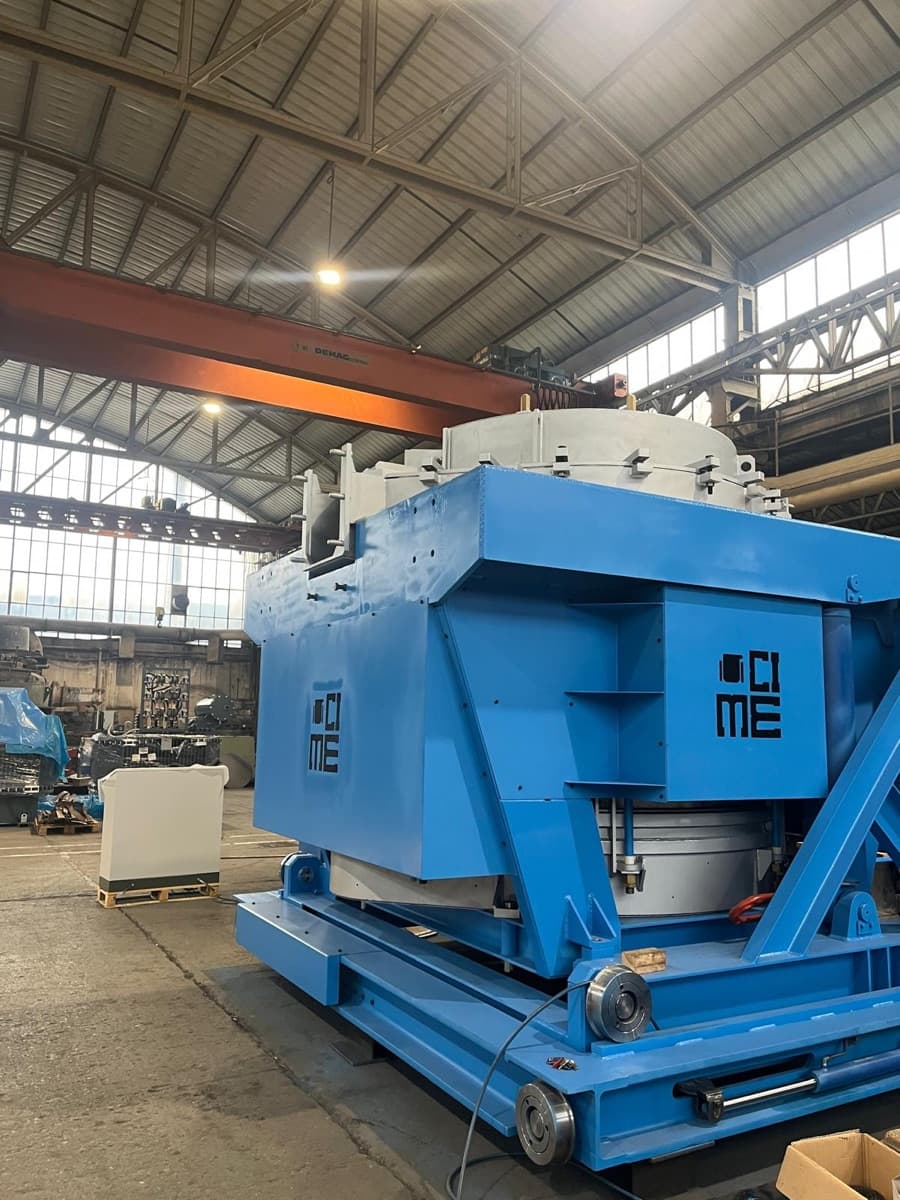
The furnace body is the muscle. At its centre is a crucible that holds the metal, wrapped in a water-cooled copper coil. The coil carries the current from the converter and turns it into the magnetic field that does the melting, while the water cooling keeps the copper from overheating under the load. The whole assembly sits on a tilting frame so that the metal, once melting is complete, can be poured out cleanly.
Key point
The converter sets how much power to deliver and at what frequency; the coil turns that power into heat in the metal. If either one is not correctly sized for the other, the melting result suffers. CIME designs both components, supplied together or separately, ensuring compatibility between the parts in every case.
From cold charge to molten metal
Let us follow one melt from start to finish. The furnace is charged with cold metal: a mix of scrap, foundry returns and fresh alloy, sized to prevent bridging in the crucible. The converter is switched on and ramps up power. At first the field couples into the solid pieces and heats their surfaces; as they soften and slump, the metal starts to turn liquid from the bottom upward until the whole charge is molten.
Once the liquid bath has formed, melting proceeds faster, because molten metal couples with the field more efficiently than a solid charge, and the electromagnetic stirring begins to circulate it, where required. More metal can be added during melt-down, so the furnace is often topped up rather than filled all at once. When the charge is fully liquid the operator raises it past its melting point to the pouring temperature.
Through all of this the temperature is measured and held under digital control. A modern system meters the power it delivers and reads the bath, so it can hold a set temperature, correct chemistry with a measured addition, and tell the operator exactly where the metal stands. When the metal is on temperature and in specification, the furnace tilts and pours, into a ladle or into a transfer system.
Why foundries melt this way
Set against the older ways of melting, induction offers a consistent set of advantages, and they all follow from the same fact: the heat is made inside the metal, electrically, with nothing burning. Five of them matter most on the foundry floor.
| Advantage | What it gives the foundry |
|---|---|
| Superior metal quality | No combustion products reach the melt, so the metal stays clean and consistent |
| Clean, low-emission process | Heat comes from the magnetic field, not a flame, with no burning and no flue gas from the melt |
| Full scrap recovery | Scrap and returns melt down and are corrected in the bath, so the whole charge is usable |
| High energy efficiency | The heat is generated directly in the metal, not in a furnace and flame around it |
| Precise temperature control | Digital control of the molten metal holds the pouring temperature and keeps castings consistent |
Read all together, these are why induction has become widespread in foundry melting. Metal quality comes first: with no combustion products to pick up, the molten metal stays clean, and a bath that is stirred (if required) and evenly heated is easy to sample and correct. The clean process follows, no flame and no flue gas from the melt itself, a better shop environment and a smaller footprint. Full scrap recovery lets a foundry charge its own returns and bought scrap; melting in the crucible makes it possible to correct the chemistry. Energy efficiency comes from the fact that the heat is generated directly in the metal instead of heating the metal inside the furnace with a flame. And precise temperature control, through the digital converter, keeps the bath on temperature, so that the pour is on temperature and the castings are consistent.
The heat is made inside the metal, electrically, with nothing burning. Many of the advantages of an induction furnace follow from this idea.
Almost all foundry melting today is done in coreless induction furnaces, in which the coil surrounds a crucible and heats the entire bath together; the furnace empties completely and the alloy can be changed easily. CIME has engineered coreless induction furnaces in Turin since 1952, from the melting furnaces themselves to their IGBT power supplies. To learn about the technology behind them, start with the core technology.
Frequently asked questions
How does an induction furnace work?
An induction furnace melts metal with a magnetic field rather than a flame. A converter turns mains electricity into a medium-frequency alternating current, a water-cooled copper coil around the crucible turns that current into an alternating magnetic field, and the field induces eddy currents inside the metal charge. Those currents heat the metal from within by its own electrical resistance, so it melts without any combustion or contact with a burner.
What is the working principle of induction melting?
The principle is electromagnetic induction, described by Michael Faraday in 1831: a changing magnetic field induces an electric current in a nearby conductor. In a furnace the coil's alternating field induces circulating eddy currents in the metal, and the metal's resistance to those currents turns the electrical energy into heat directly inside the charge. The same field also stirs the molten bath, which mixes the melt and evens out its temperature and composition.
What are the main parts of an induction furnace?
Two main components do the work. The power converter, usually an IGBT medium-frequency unit, is the brain: it conditions the mains supply into the frequency and power needed by the coil, which then melts the metal. The furnace body is the muscle: a water-cooled copper coil wound around a crucible that holds the charge, mounted on a tilting structure so that the molten metal can be poured.
Why do foundries use induction furnaces?
Because induction melting is clean, efficient and controllable. The heat is generated directly in the metal with no combustion, so there are no flue gases and no contamination from a fuel, the whole charge including scrap can be recovered and corrected in the bath, and digital control holds temperature precisely. Together these give high metal quality and high energy efficiency, which is why induction is now widely used in modern foundries.
What is a coreless induction furnace?
A coreless induction melting furnace consists of a coil that surrounds a crucible, so the whole bath is melted together and kept uniform. It empties completely by means of the tilting structure in which the crucible sits. An alternative is the rotary combustion (gas) furnace, which uses a direct flame or a burner to heat a crucible holding the metal. In that furnace the chemistry of the metal is not corrected during melting.
References and sources
- Foundry Trade Journal, technical article on coreless induction melting, 2006.
- Cast Metal Times, coreless induction furnace practice, 2004.
- CIME S.r.l., internal engineering documentation on induction melting and IGBT power supplies, Turin.