Key takeaways
- An automatic pouring system fills every mould on a moving line to the same weight without an operator pouring by hand from a ladle, so scrap, labour and safety all improve over hand pouring.
- There are two families: an automatic pouring ladle, which tips a measured ladle, and a heated press-pouring buffer, which holds the metal sealed and hot and pushes a metered stream under inert pressure.
- Choose by the metal and the line first. Ductile iron on an automatic line needs a heated, sealed pouring furnace that holds magnesium and temperature. Automatic lines in general gain considerable benefits from using the CAP.
- The control layer decides repeatability: stopper-rod metering, electro-optical vision of the pour, auto-centering to the line and real-time weighing make every casting extremely precise. CIME builds the CAP, the world's first automatic coreless press-pouring furnace, since 1976.
What an automatic pouring system is
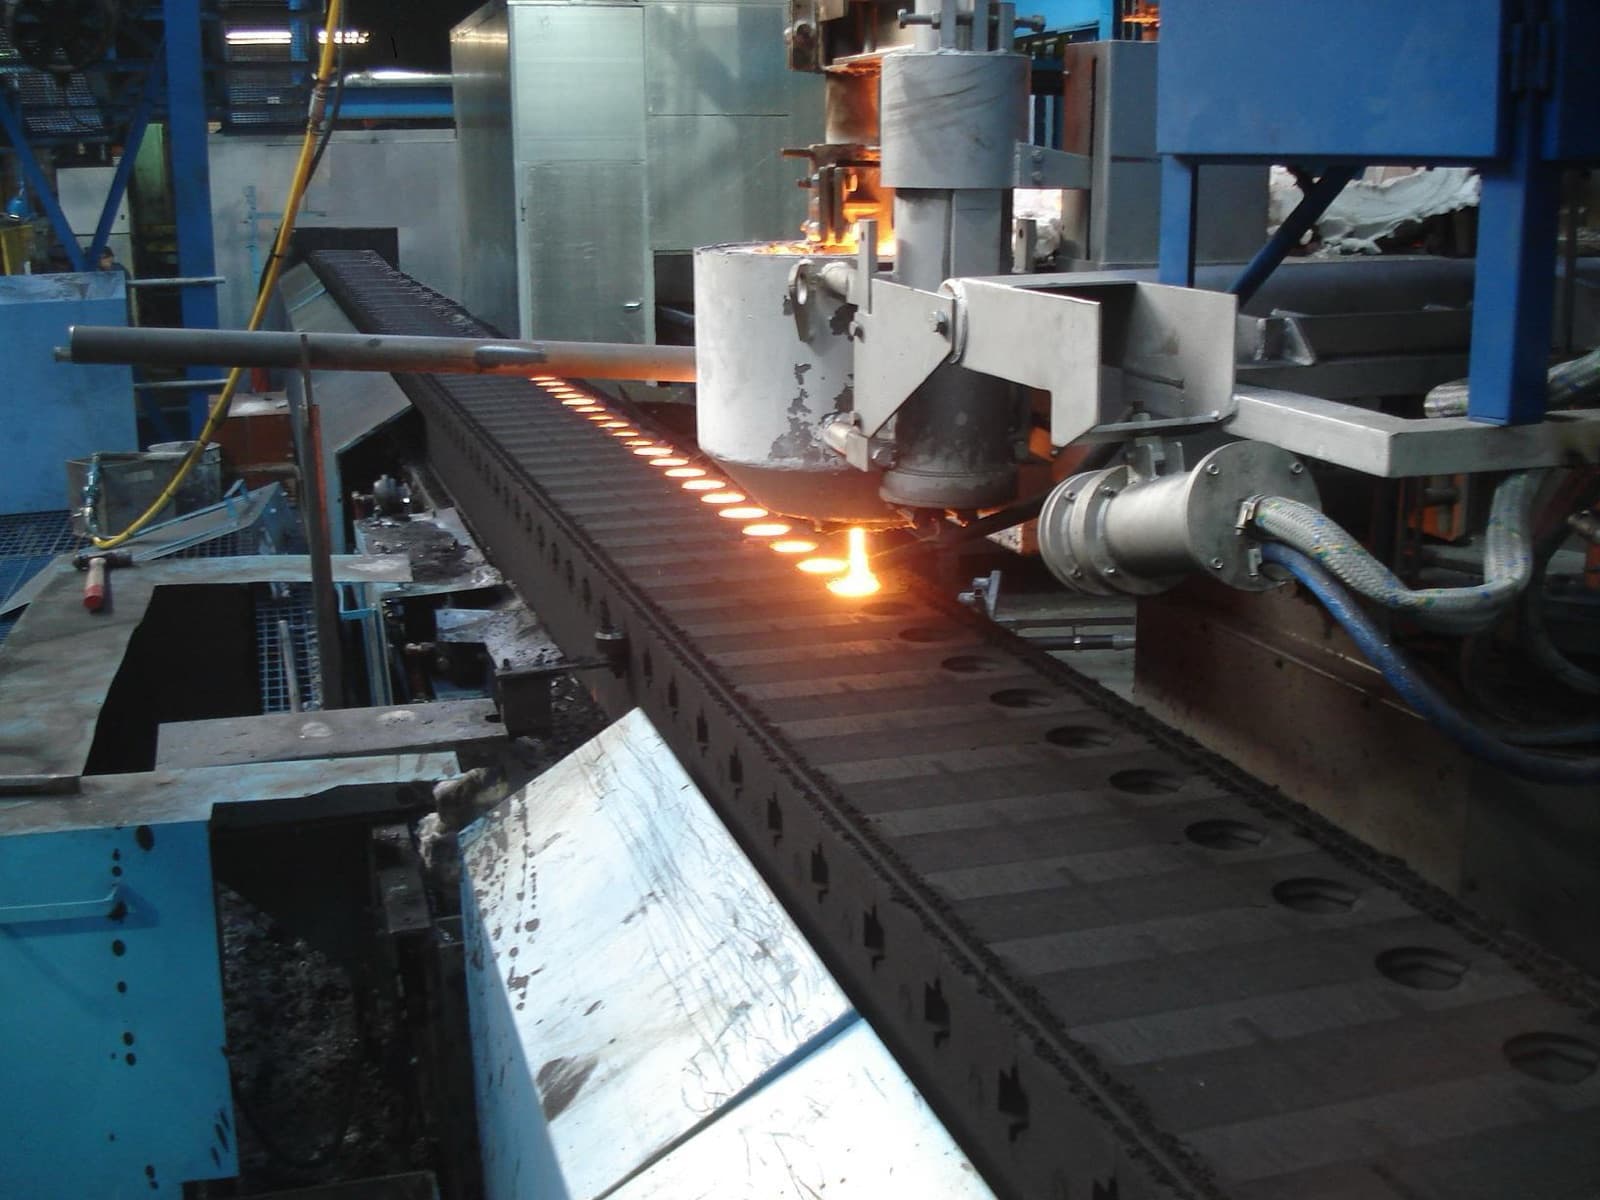
An automatic pouring system fills every mould on a moving line with molten metal without an operator pouring by hand from a ladle. Our camera frames the pouring cup and sends a continuous signal to the stopper. The flow rate adapts in real time to the filling profile of every mould and keeps the pour aligned with the line as the moulds move. In a modern foundry this job is no longer done by a person with a ladle: it is a machine that pours the same way every time.
Foundries automate the pour for four reasons that compound: less scrap, because a metered stream fills consistently and keeps slag out of the casting; more throughput, because the pour keeps pace with an automatic moulding line instead of setting it; lower labour and better safety, because the operator is away from the furnace in a control booth; and tighter chemistry, because the metal is always ready at the right analysis and temperature.
Put together, those gains are the payback case. Less scrap and higher yield mean more good castings from the same melt; steadier throughput means the pour stops setting the pace of the line; and holding the metal ready instead of remelting it saves energy every shift. A buyer chooses an automatic pouring system to improve those points, so the useful question at every stage is: which choice improves them most for a given metal and line?
Note
An automatic pouring system sits between the melt and the moulding line and handles the metal on its way to the mould. The choice of system determines how the metal is held and metered: this is where a fundamental part of pouring quality, scrap reduction and production continuity is decided.
Two families of automatic pouring
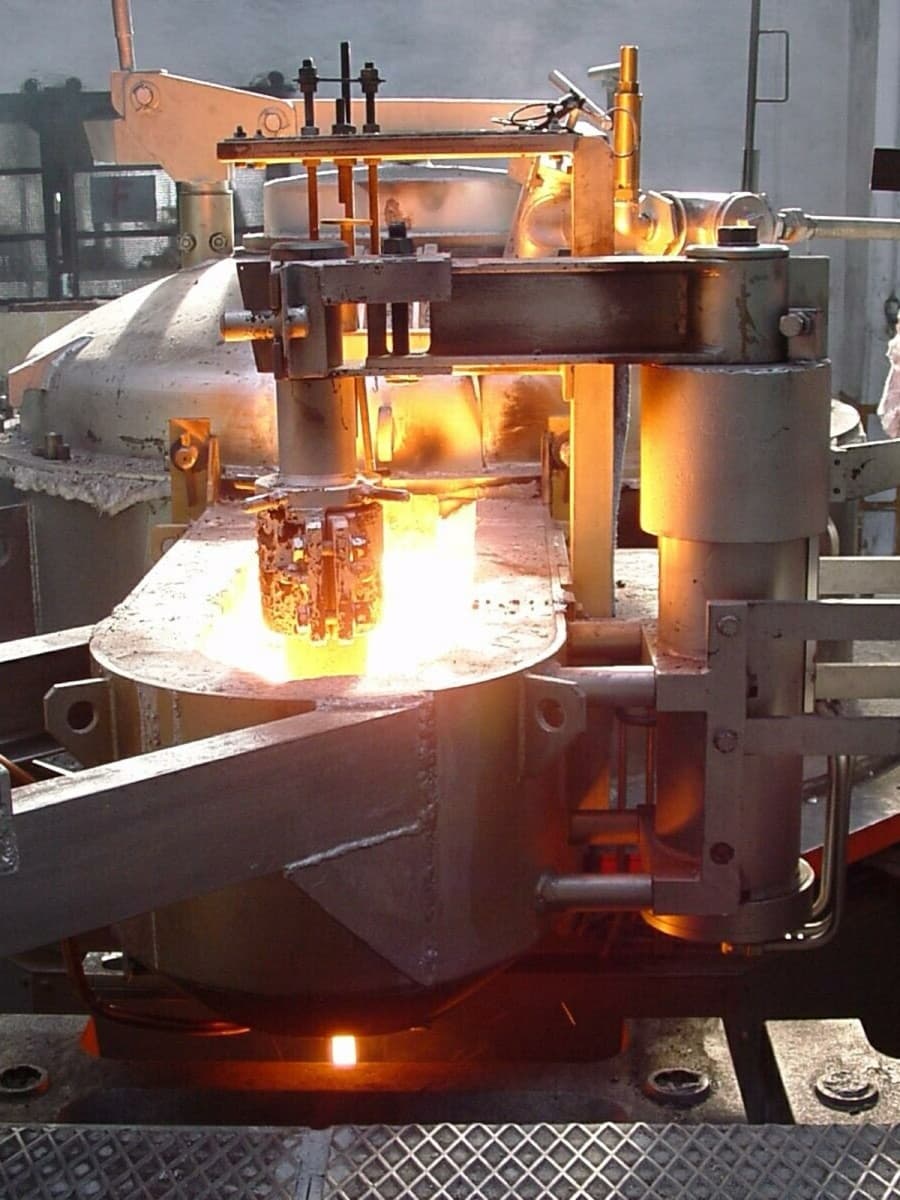
There are two established ways to automate the pour. An automatic pouring ladle tips the metered metal over each mould: the vessel cools and its slag travels with the stream, but the tipping is automated. A heated automatic press-pouring furnace does the opposite: it holds the metal in a sealed, heated furnace and pushes a metered, slagless stream out under inert nitrogen pressure, so the metal does not cool and is cleaner.
Ladle pouring and automatic pouring have different characteristics and operating modes, which affect how the metal is handled and the pouring parameters. For a more detailed comparison of the two systems, see the article press pouring vs ladle pouring. For more detail on how a press-pouring furnace works, see press-pouring, explained.
Why choose the CAP
Seven key concepts for understanding which system to choose.
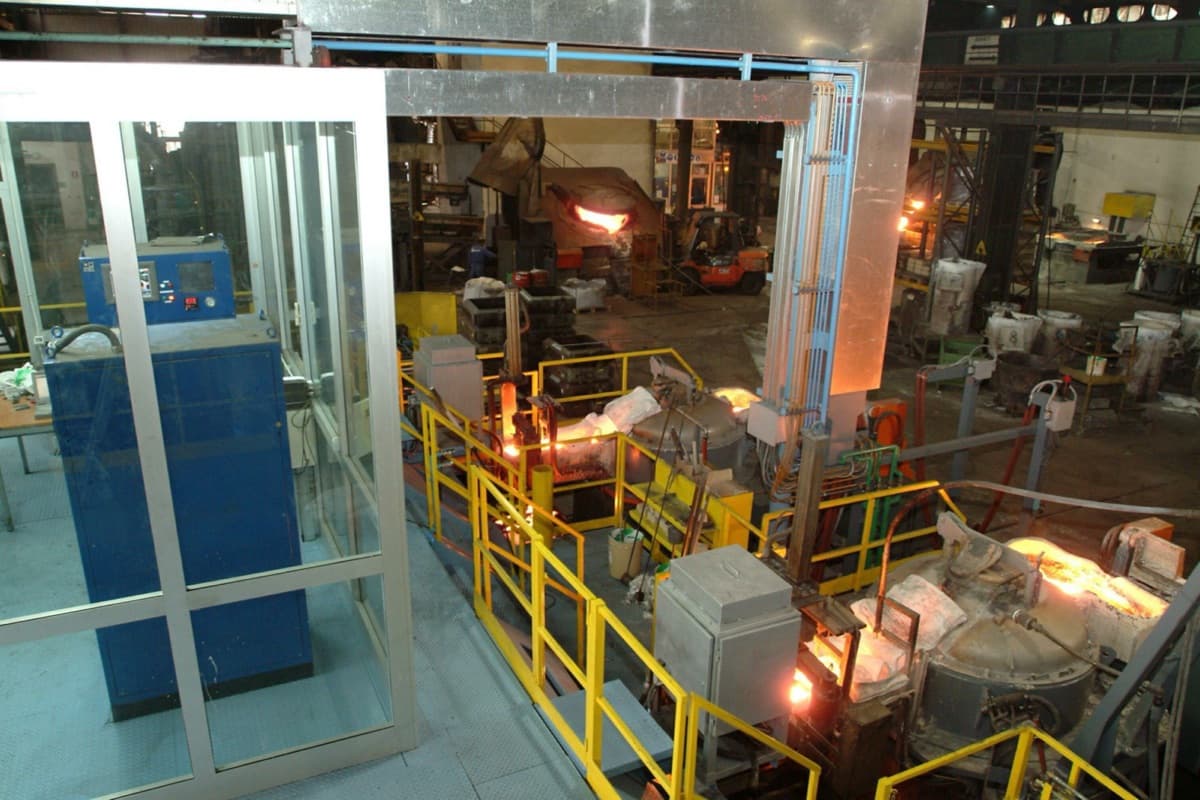
- The metal. With the CAP you can pour any ferrous or non-ferrous alloy: grey iron, ductile iron with 100% reliability, steel, copper-based alloys (bronze and brass) and light alloys including aluminium. For ductile iron in particular, nitrogen pressurisation preserves the magnesium content, and lower treatment temperatures improve metallurgical quality and reduce the amount of alloy needed.
- Match the system to the line. An automatic moulding line, vertical Disamatic or horizontal, needs a metered, repeatable pour that fills every mould to the same weight. A low-volume or jobbing line may be served by a simpler pouring ladle.
- Specify temperature control. The CAP holds the pouring temperature between casts and can superheat quickly. An unheated ladle loses heat in transit and forces a hotter tap upstream, which costs energy and stresses the refractory.
- Specify pour control. The CAP combines stopper-rod metering with a closed-loop optical vision system that reads the mould pouring cup and trims the flow in real time, so casting weight stays constant as the line varies.
- Specify automation and repeatability. With the CAP you can auto-center on the moulding line and run the pour in teach-in mode. The system records the validated pour and repeats it automatically, mould after mould, for maximum repeatability without an operator at the controls.
- Specify metal quantification. The CAP features real-time weighing of the bath, which lets the shop know exactly how much metal is left, instead of estimating from level.
- Emptying and flexibility. The CAP can be emptied completely by tilting it backwards, which makes it easier to change metal type. This removes the need for a metal heel, allowing quick, simple alloy changes.
Depending on production needs, the pour can run in three different modes: let's look at them in detail.
Automation and control: how the CAP is a complete pouring system
The precision of a pouring machine depends on the system that controls it. On the CAP, this control is organised into three modes. Joystick is manual control. Teach-in records a correct pour and repeats it mould after mould. Optical is the most advanced level: the Optical High-Speed Vision system, an electro-optical control developed by CIME, monitors the mould and signals the stopper in real time to open and close and pour the right amount of metal into every mould. The result is constant filling weight. Each mode is a further step in autonomy for the foundry.
Alongside this pour control sit two more CAP systems. Auto-centering receives the pouring position from the moulding line and moves the furnace (right-left; forward-back) to position itself correctly and stay aligned with the mould. Real-time weighing tracks how much metal is in the furnace so metal refill requests and grade changes are planned. Together they turn a furnace into a pouring system that holds temperature, meters the stream, follows the line and keeps every casting on weight, which is what the buyer is really specifying. For where this control layer sits in the wider platform, see the core technology.
Fitting it to your line
Specifying the system is half the job; fitting it to the shop is the other half. Three practical questions decide how cleanly an automatic pouring system drops into an existing line.
First, how the CAP is charged. A press-pouring furnace is refilled from the melting furnace between casts, by transfer ladle or by an automatic skip-loading system that lifts and tips the ladle into the pouring furnace under controlled motion, so the CAP is topped up without ever interrupting the pour. A larger transfer ladle means fewer charging cycles and a steadier line.
Second, how the system talks to the moulding line. The pour has to follow the moulds, so the system moves (right-left; forward-back) to take the pouring position from the line, and it starts, stops and meters in step with the line cycle.
Third, footprint and retrofit. A pouring system has to fit the existing layout and the existing line, so the question is not only performance but whether it can be installed without rebuilding the shop. Our modern system is engineered to sit on the line it serves, with the operator moved off the metal and into a control booth, and to be specified around the equipment a foundry already runs.
When a simpler system is enough
Not every line needs a heated, sealed buffer. A shop running short batches at low daily tonnage, with frequent unrelated alloy changes on a single line, can be well served by an automatic pouring ladle. The CAP system earns its place where the metal is demanding and the volume is steady, for ferrous and non-ferrous metals and on an automatic line above all.
Key point
Match the system to the process, not the process to the system. Specify the metal and the line first, then the controls that keep the pour repeatable, and the right family: ladle or heated automatic press-pouring furnace.
Frequently asked questions
What is an automatic pouring system?
An automatic pouring system delivers a controlled, repeatable stream of molten metal into each mould on a moving line without an operator pouring the metal by hand from a ladle. It meters the pour precisely so every mould is filled to the same weight.
How do I choose an automatic pouring system for my foundry?
Start from the metal and the line. Ductile iron on an automatic moulding line needs a heated, sealed buffer that holds magnesium and temperature, while low-volume production that needs less precision can be served by a simpler pouring ladle. Then specify temperature control, pour control (stopper-rod metering with optical vision), automation such as auto-centering, real-time weighing and full emptying for fast grade changes.
Do I need a heated pouring system, or is an automatic pouring ladle enough?
It depends on the metal, the volume and the line. A heated press-pouring buffer holds the pouring temperature and fills every mould identically at high volume. An automatic pouring ladle is simpler and can suit short runs or low tonnage.
How does an automatic pouring system keep every casting on weight?
The stopper-rod system meters the flow while CIME's Optical HSV (High Speed Vision) system frames the pouring cup and sends a continuous signal to the stopper-rod control, so the flow rate adapts in real time to the filling profile of every mould. Auto-centering keeps the pour aligned with the moving moulds, the teach-in pouring mode repeats a validated pour, and real-time weighing tracks how much is in the furnace.
Can an automatic pouring system be installed on an existing moulding line?
Yes. Our modern CAP automatic pouring system is engineered to fit the line it serves, so it can be installed on an existing automatic moulding line without modifying the shop.
References and sources
- Foundry Trade Journal, technical article on automatic press-pouring, 2006.
- Cast Metal Times, coreless induction and pouring practice, 2004.
- CIME S.r.l., internal process documentation on CAP automatic pouring, Turin.