Key takeaways
- Press-pouring pours by pressure, not by tilting. Inert gas pressure pushes the melt up a discharge duct and out as a clean, metered stream.
- The bath sits in a sealed crucible. An elliptical induction coil holds the bath and both ducts at temperature, so nothing freezes between pours.
- More than 90% of the bath is poured by pressure and the furnace empties 100% by back-tilting, leaving no ballast heel.
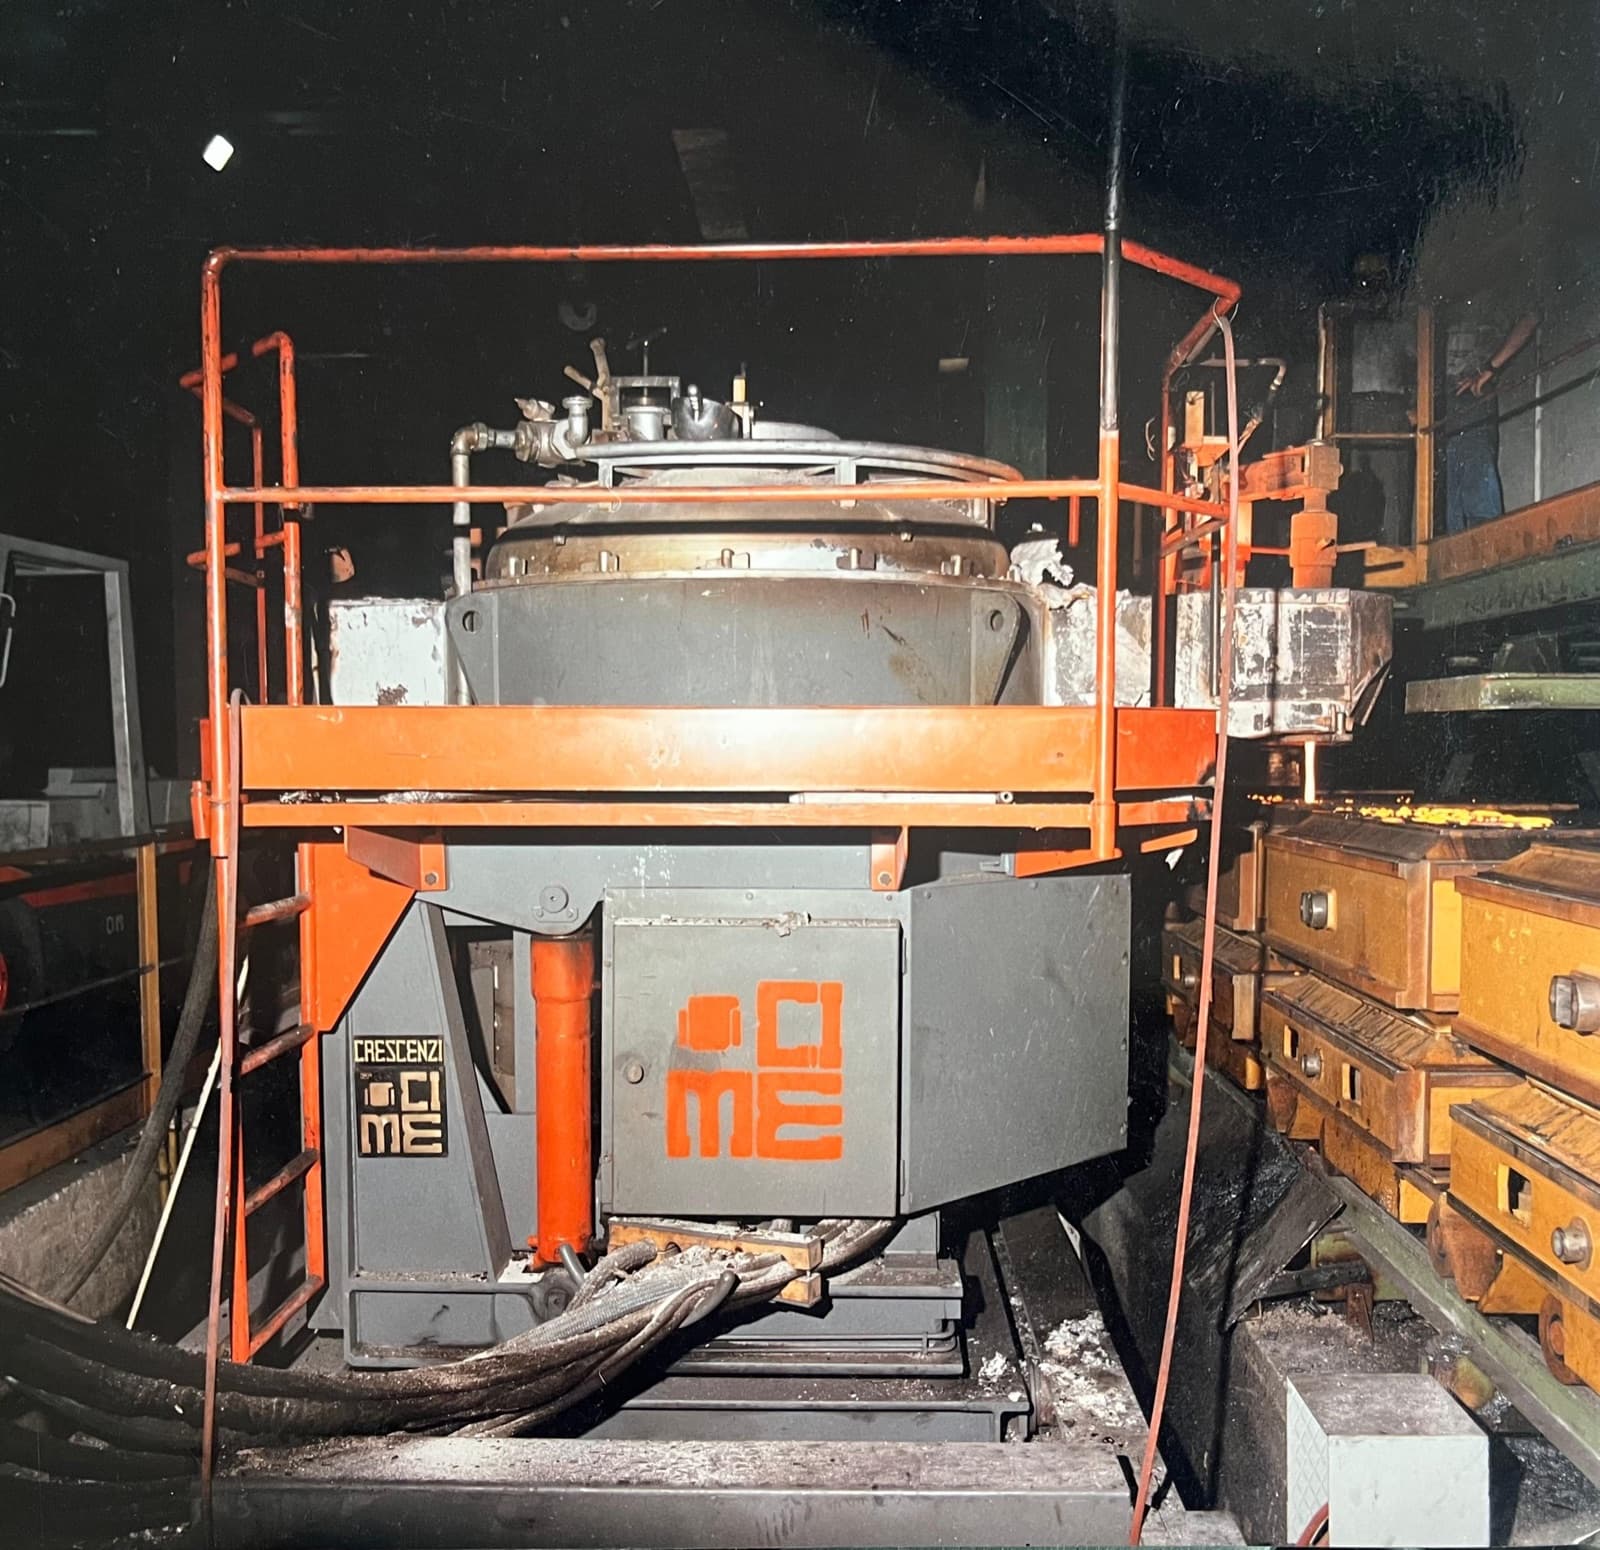
- CIME built the world's first automatic press-pouring furnace, in production since 1976.
How the pour works
An automatic press-pouring furnace works differently from a tilting ladle: while the ladle pours by tilting its own body, the CAP drives the metal out by gas pressure. The molten metal is held inside a sealed coreless crucible. An elliptical induction coil wraps both the crucible and the two siphons, ensuring uniform heating throughout the system. This way the siphons neither cool down nor become encrusted with slag.
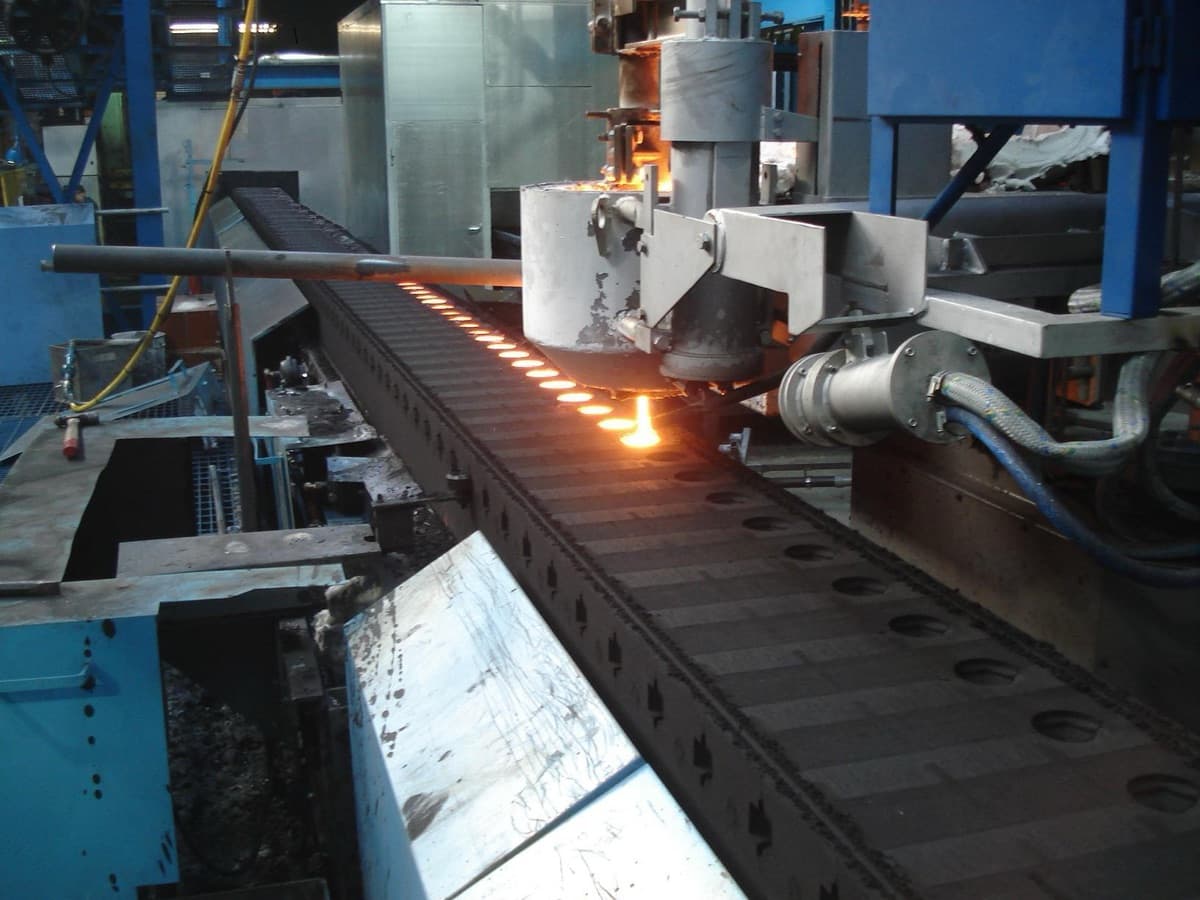
To pour, an electro-pneumatic system raises inert nitrogen pressure inside the crucible. The pressure pushes the melt up the pouring siphon; the stopper-rod meters the flow, ensuring a precise, continuous stream. Because the metal is poured through the nozzle at the bottom of the pouring spout, while the slag floats on the surface, the pour comes out clean and slagless. The metal level in the pouring spout is held constant by pressure regulation regardless of how full the furnace is, so the first mould and the last mould of a batch are filled identically.
Note
The principle is coreless induction throughout. The same technology that lets a coreless furnace melt and hold the bath at temperature is what allows the CAP to pour at a controlled temperature. CIME has built CAP pouring furnaces on this principle since 1976.
Press-pour vs an unheated system
Compared with an unheated or ladle-fed pouring system, a heated press-pour furnace is a buffer that is always ready and always at temperature.
The difference shows up where it counts: scrap rate, alloy chemistry and line uptime.
The metal in the CAP is always held at the correct pouring temperature: if the line stops, there is no need to scrap the bath or remelt it, because the furnace simply keeps it on hold.
Reliability, precision and constant temperature: every pour is the same as the one before.
Pouring control and furnace emptying
The CAP escalates through three control modes. Joystick is manual, for setup and emergencies. Teach-In records a good pour once, then repeats it mould after mould. Optical is the mode in which a camera frames the pouring cup, feeding a continuous signal to the stopper-rod control. The flow rate adapts in real time to the filling profile of each mould. The result is a precise, continuous pour onto any automatic moulding line, vertical Disamatic or horizontal alike.
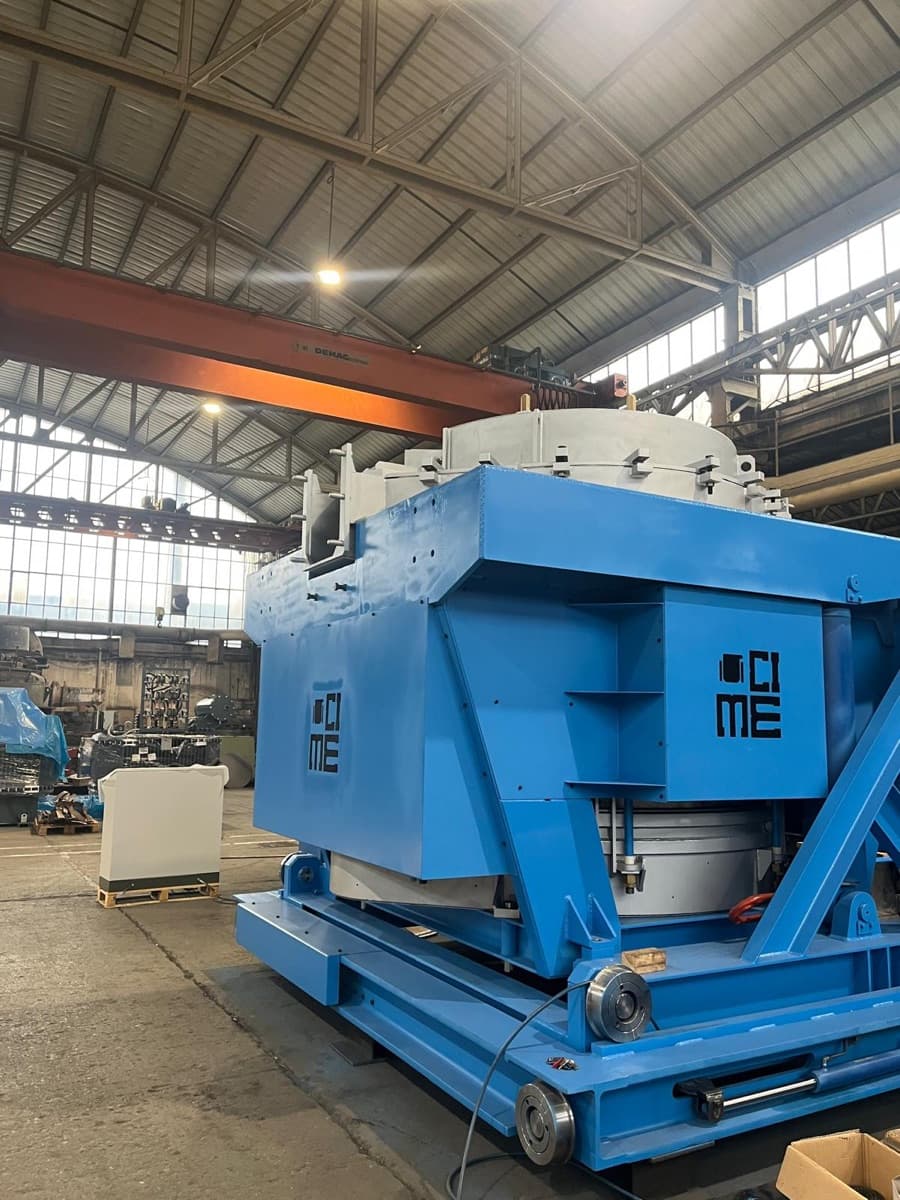
Emptying the furnace is also handled in a controlled way. More than 90% of the metal can be discharged using pressure, without tilting. In addition, the CAP furnace can be tilted backwards by up to 90°, so the crucible can be emptied completely, leaving no metal residue inside.
Benefits for foundry production
The practical payoff is repeatable castings with less scrap and less waste. A heated, sealed buffer keeps the metal in spec, fills every mould to the same weight and never forces a remelt when the line stops. With the CAP, pouring is automatic and the furnace can easily be emptied, by tilting through 90°, for the necessary alloy changes.
Key point
The CAP works on the press-pouring principle and consists of a single crucible that performs the functions of melting, holding and pouring, operating under inert cover. The metal level in the pouring spout is held constant from the first mould to the last, ensuring a continuous, uniform process.
Frequently asked questions
What makes a press-pouring furnace different from a tilting ladle?
A tilting ladle tilts its own body to pour the metal. In the CAP, an automatic press-pouring furnace, the pressure of the inert gas pushes the melt up the pouring siphon, where the stopper-rod meters a precise pour onto the line.
Why does press-pouring keep ductile iron in spec?
The bath is held under inert nitrogen cover and kept at temperature by the coil, so magnesium fades far less while the metal waits.
How much of the bath can a CAP discharge?
More than 90% of the bath is discharged by pressure alone, and the furnace empties 100% by back-tilting, so there is no ballast heel of metal left trapped inside between casts or alloy changes.
References and sources
- Foundry Trade Journal, technical article on automatic press-pouring, 2006.
- Cast Metal Times, coreless induction and pouring practice, 2004.
- CIME S.r.l., internal process documentation on CAP press-pouring, Turin.